A VNA truck operating at full lift height does not forgive a poor floor detail. The question, do VNA floors need joints, has a direct answer: concrete floors need a strategy for movement and shrinkage, but joints must be designed, located, and finished to protect very narrow aisle operations. A conventional joint layout can undermine a superflat floor before the facility is fully operational.
For warehouse owners, general contractors, and operations teams, this is not a cosmetic issue. Joint-related defects can affect truck stability, mast movement, load handling, rack clearances, wheel wear, and maintenance costs. The correct approach is not simply to eliminate every joint. It is to control where joints occur and ensure they do not compromise the defined traffic paths.
Do VNA Floors Need Joints?
Yes, most VNA floors require joints of some kind. Concrete shrinks as it cures. It also responds to temperature changes, moisture conditions, restraint from walls or columns, and construction sequencing. If that movement is not managed, the slab will crack unpredictably.
What VNA floors do not need is a standard grid of saw-cut control joints running through critical forklift travel lanes. In a conventional slab-on-grade, regularly spaced contraction joints encourage cracking to occur at planned locations. That approach may be acceptable for general warehouse traffic. In a VNA aisle, however, every transverse joint represents a potential disruption under a narrow-aisle truck.
At elevated lift heights, minor variations at floor level become more significant at the top of the mast. A joint that has opened, curled, spalled, or settled can create a repeated impact point. That impact affects the truck, the operator, the load, and the long-term condition of the aisle.
The design objective is therefore controlled movement with minimal interruption to VNA truck wheel paths. Depending on the facility, this may involve a jointless floor design, large-pour construction, carefully located construction joints, or a hybrid solution that combines different floor zones.
Why Joint Location Matters in Very Narrow Aisles
A VNA floor is a working component of the material-handling system. It must support the specified truck type, rack configuration, guidance method, wheelbase, load profile, and lift height. Flatness and levelness are not general quality measures in this environment. They are operational requirements.
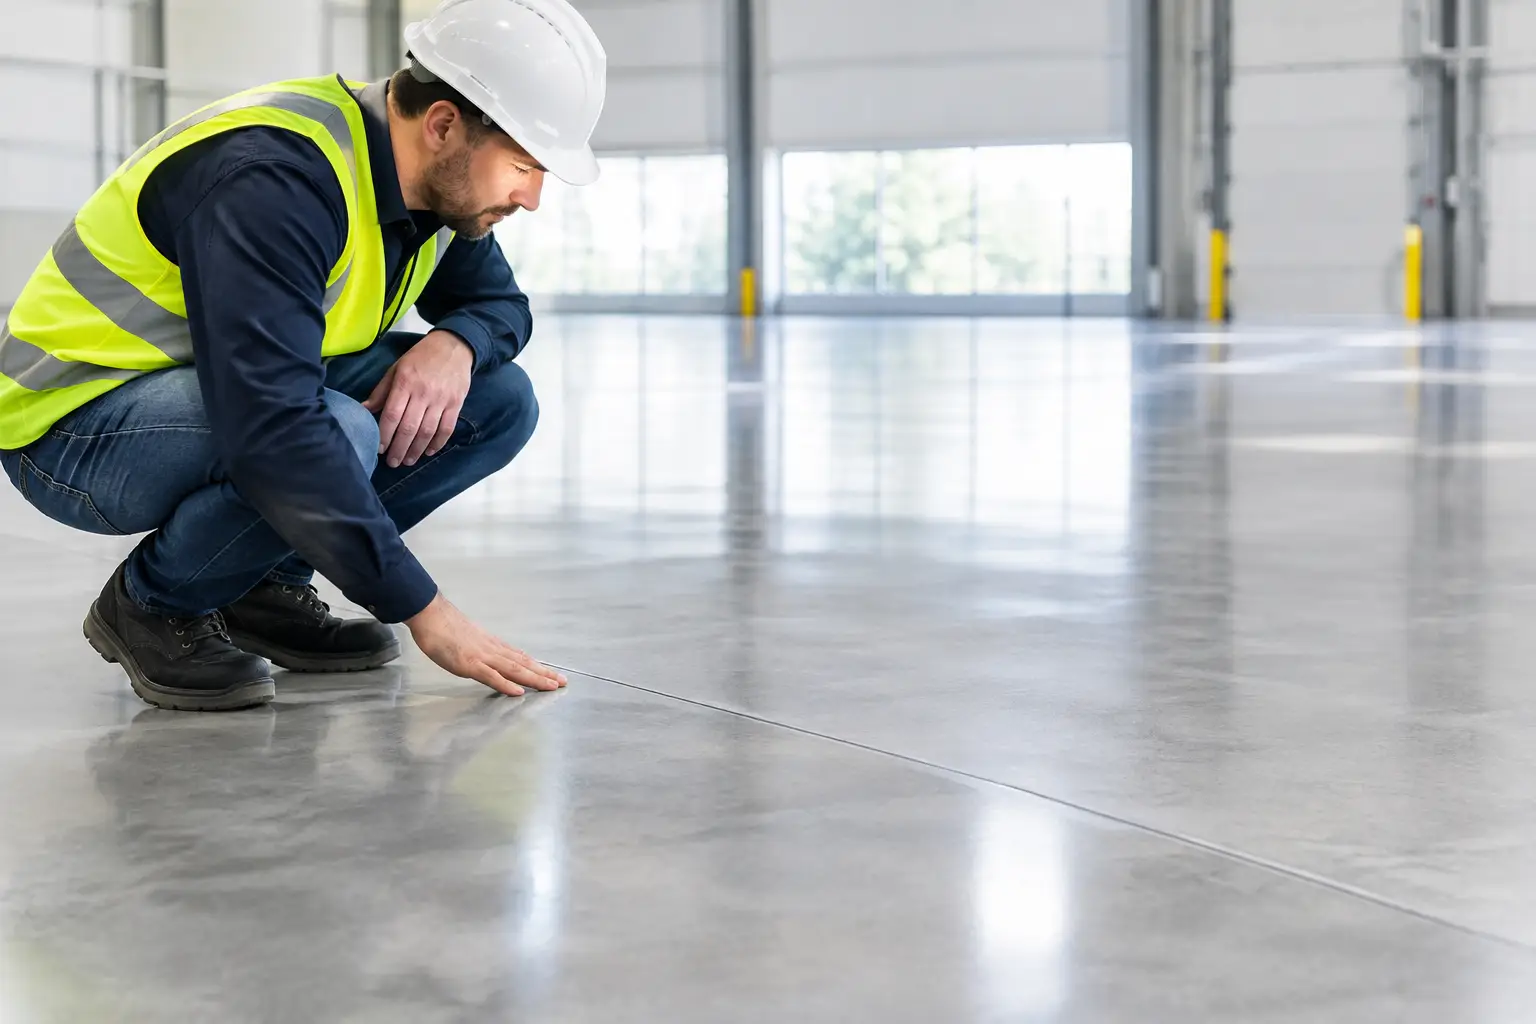
A joint crossing an aisle can create several problems. The joint may open as the slab shrinks, leaving a gap that subjects wheels to impact. The edges may curl upward or break down under repeated loading. Differential elevation can develop across the joint. Even a joint that appears acceptable at handover can deteriorate under concentrated forklift traffic if it was not designed and protected for the application.
Joint placement also matters outside the aisle. Joints near rack legs, transfer zones, end-of-aisle turning areas, battery rooms, and dock approaches require separate consideration. These areas may see different loading, turning forces, and moisture exposure than the main VNA aisles.
The right floor plan starts with the material-handling layout, not a generic concrete joint pattern. A floor contractor should understand where each truck travels, where it turns, where it stops, and how the floor will be measured and accepted.
Joints are not all the same
The term “joint” can describe several different details, and each serves a different purpose. Contraction joints manage shrinkage cracking. Construction joints occur where separate concrete placements meet. Isolation joints separate the slab from walls, columns, equipment bases, or other restrained elements. Expansion or movement joints accommodate anticipated movement between structural elements.
Treating these details as interchangeable is a common source of specification and field errors. A VNA floor may be designed with very limited contraction joints in operating aisles while still requiring construction and isolation joints at planned locations. The project team must coordinate those details before placement begins.
Jointless Does Not Mean Crack-Free
Jointless flooring is often the preferred direction for superflat VNA aisles because it reduces interruptions in the defined travel path. But “jointless” should not be interpreted as “free of all joints” or “incapable of cracking.” It generally means the floor is designed to reduce or eliminate saw-cut contraction joints within critical operational areas.
A successful jointless design relies on disciplined engineering and installation. The slab thickness, reinforcement approach, concrete mix, fiber dosage where applicable, subbase condition, pour size, placement sequence, curing method, and environmental controls all influence performance. The details must be selected for the project rather than copied from a previous warehouse.
Jointless construction has trade-offs. Larger placements demand strong planning, adequate crew capacity, dependable concrete supply, and precise finishing control. Shrinkage must still be managed. If the design or execution is weak, cracks can develop in locations that are harder to predict and repair than planned joints.
For this reason, a jointless VNA floor is not a shortcut. It is a high-control construction method intended to support high-control operations.
How VNA Floor Joints Should Be Planned
The first decision is whether the project is new construction, an expansion, or an upgrade to an existing operational floor. New construction provides the greatest opportunity to align the slab design with the rack and truck layout. Existing facilities require a detailed survey to determine what can be corrected through grinding, repair, or traffic-layout changes.
Where joints cannot be avoided, they should be placed away from critical wheel tracks whenever practical. In some layouts, joints can be coordinated with rack lines, aisle boundaries, or other locations that reduce direct truck impact. Construction joints that must carry regular traffic may require purpose-designed edge protection and a repairable joint system suited to the loading profile.
Joint spacing cannot be selected from a rule of thumb alone. The correct spacing depends on slab geometry, restraint, reinforcement, concrete behavior, environmental exposure, and placement strategy. The flatness requirement must also be defined in a way that reflects the actual VNA travel path. General floor numbers may not establish whether a floor will perform under a specified narrow-aisle truck at operating height.
Early coordination matters. The structural engineer, concrete designer, rack supplier, VNA truck supplier, guidance-system provider, general contractor, and flooring specialist should be working from compatible information. Late changes to aisle widths, rack locations, wire guidance, or pour breaks can create expensive corrections.
Wire guidance requires floor coordination
Wire-guided VNA systems add another layer of coordination. The guidance wire is installed in a precisely cut groove, usually along the center of the aisle. That groove must be accurately located, cleanly cut, properly filled, and protected from failure under traffic.
Wire guidance does not eliminate the need for a flat floor or sound joints. In fact, it makes alignment and execution more visible. A truck may be accurately guided laterally while still experiencing vertical disturbance from a poorly performing joint. The guidance installation, aisle flatness, and joint plan must work as one system.
Existing VNA Floors Can Often Be Improved
An existing floor with joints in the aisles is not automatically a replacement project. The proper response depends on the level of distress and the operating requirement. Some facilities benefit from precision grinding to improve profile conditions. Others require joint rebuilding, edge repair, resinous joint fillers, or localized slab remediation.
Floor and joint repair must address the cause, not only the visible damage. If a joint is spalling because of repeated wheel impact, a surface patch alone may fail quickly. The repair may need to restore the joint arris, rebuild the damaged concrete, protect the edges, and accommodate the movement the joint was intended to manage.
Grinding can improve localized high spots and correct certain flatness issues, but it cannot solve every structural or joint-related condition. Excessive grinding may reduce cover, expose aggregate, or create unacceptable transitions if it is not planned against a verified survey. The best repair scope begins with measured data, traffic observations, and a clear understanding of the required outcome.
For active facilities, repair sequencing is equally important. Work should be organized around operating windows, aisle closures, cure times, material staging, and safe return-to-service requirements. Downtime is part of the project cost. A repair that meets the technical requirement but disrupts production unnecessarily is not a complete solution.
Specify Performance, Not Just a Joint Pattern
A VNA flooring specification should state the operational performance required, then define the construction and verification methods needed to achieve it. Simply calling for “superflat concrete” without identifying the truck, guidance method, rack geometry, measurement standard, and traffic paths leaves too much to interpretation.
The specification should establish who is responsible for coordinating the slab layout, how floor compliance will be tested, what areas will be measured, and how defects will be corrected. It should also identify acceptable joint locations and the protection required at joints exposed to forklift traffic.
This approach gives project teams a measurable basis for quality. It also prevents a common problem: a floor that meets a broad concrete specification but performs poorly when VNA equipment enters service.
Osis Group approaches VNA flooring as an operational surface, not a standard slab. The required result is a floor that supports safe truck movement, protects high-bay storage operations, and holds its performance under sustained industrial use.
A VNA floor does not succeed because it has no visible joints. It succeeds when its movement strategy, flatness, joint details, and repairability are aligned with the work the facility expects it to perform.


