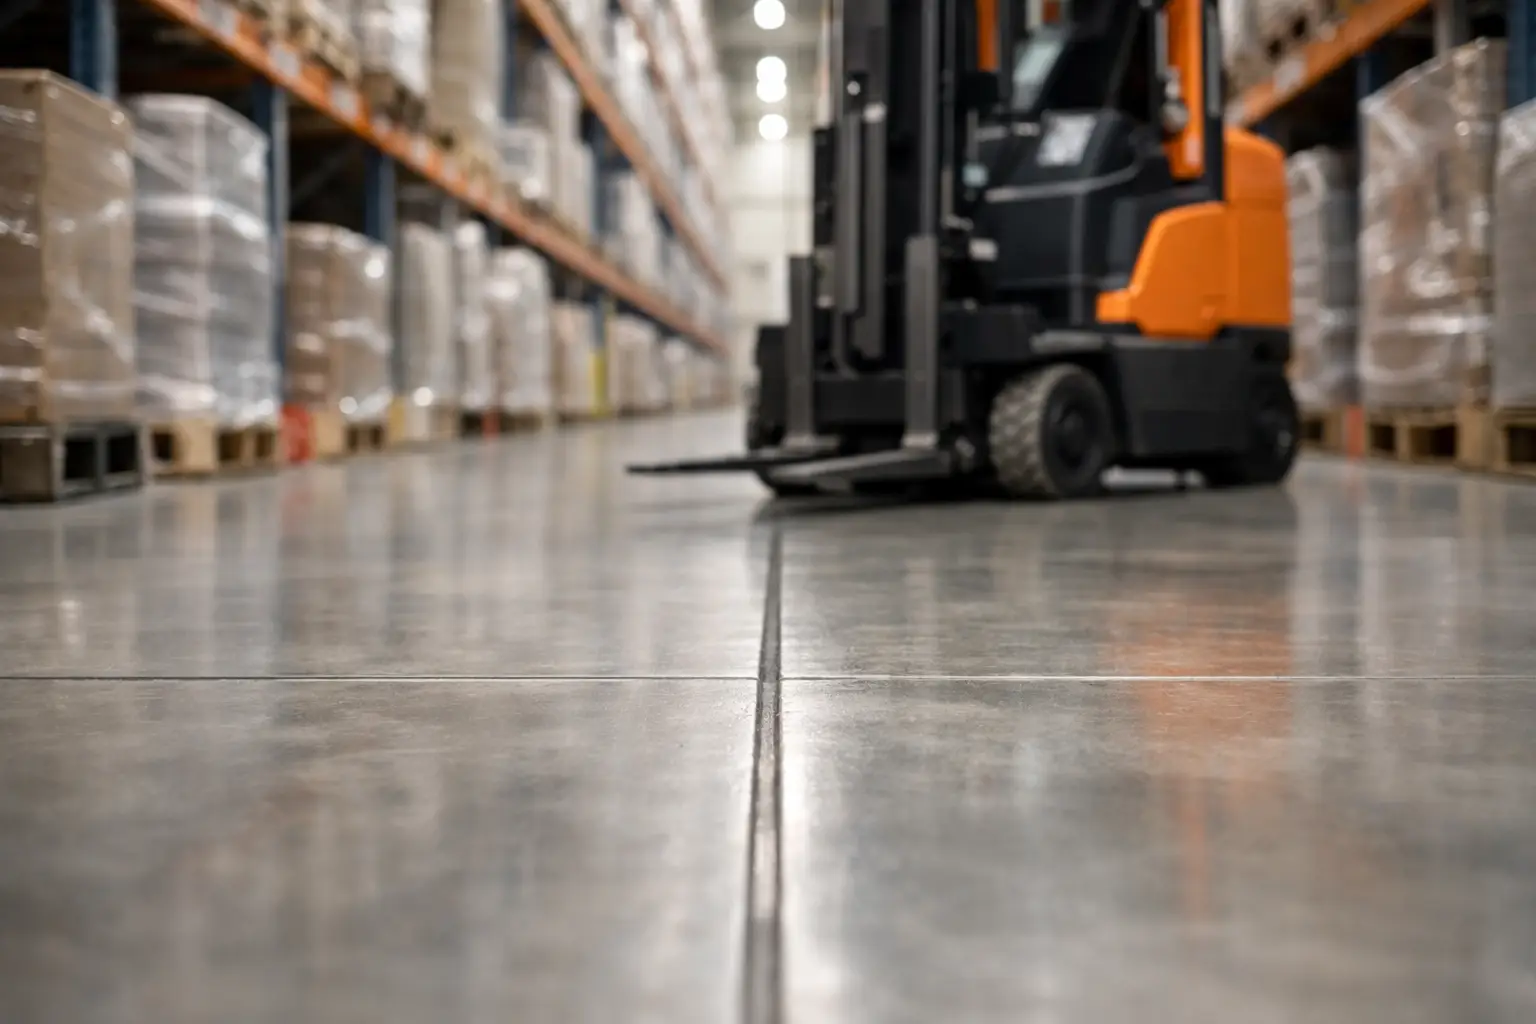
A VNA truck can operate in an aisle only inches wider than its load envelope. At that tolerance, very narrow aisle flooring is not a background construction detail. It is a working component of the material-handling system, affecting truck stability, lift height performance, rack clearance, tire wear, operator confidence, and pallet handling accuracy.
For high-density warehouses, the floor must be designed and delivered around the actual operating conditions. A conventional slab that appears flat to the eye may still create truck movement, mast sway, guidance issues, and repeated impact at rack locations. The cost is not limited to floor repair. It can include damaged product, reduced throughput, unplanned maintenance, and avoidable safety exposure.
Why Very Narrow Aisle Flooring Requires a Higher Standard
VNA operations concentrate traffic into defined wheel paths. Unlike broad-aisle facilities, where truck travel is distributed across a larger floor area, very narrow aisle trucks repeatedly run the same routes at consistent locations. Every local high point, low spot, joint fault, or surface defect is encountered again and again.
The consequence becomes more serious as lift heights increase. Small deviations at floor level can translate into greater mast movement and load displacement higher in the rack. The floor must therefore support stable travel, especially through the wheel tracks where the truck carries its load and where guidance systems operate.
This is why a general flatness result is not enough on its own. VNA floors are typically evaluated using defined-path measurements that reflect the actual truck wheel positions and travel direction. The required tolerance depends on the truck type, aisle width, lift height, wheelbase, tire configuration, rack system, and manufacturer requirements. A specification that does not account for those variables can leave the project exposed before installation begins.
Start With the Truck, Rack, and Guidance System
The strongest VNA floor projects begin with coordination, not concrete placement. The floor contractor, general contractor, rack supplier, truck supplier, and facility team need a shared understanding of the operating envelope. This includes the specified truck model, operating lift height, guided or unguided travel, aisle layout, rack tolerances, and planned traffic pattern.
Wire guidance adds another layer of precision. The guidewire must be installed at the correct position and depth, protected from damage, and tested as part of the finished system. If the wire alignment, floor profile, and truck calibration are treated as separate tasks, the warehouse can inherit a problem that is difficult and expensive to correct after racks are installed.
A clear project plan should establish who is responsible for the following before work begins:
- VNA floor tolerance criteria and the accepted measurement method
- Aisle centerlines, truck wheel paths, and rack reference points
- Guidewire routing, installation depth, testing, and commissioning
- Joint locations, joint treatment, and transitions into cross aisles
- Access, sequencing, cure time, and protection from early traffic
These decisions are practical controls, not paperwork. They prevent a floor from being judged against assumptions that were never aligned with the actual operation.
Superflat Performance Is Built in the Details
A superflat VNA floor is the result of disciplined surface preparation, placement control, finishing, measurement, and corrective work where needed. It cannot be reliably achieved by adding a high-performance coating over an unsuitable substrate. The slab profile below the finish matters.
For new construction, execution starts with stable subgrade conditions, accurate formwork, controlled concrete placement, and a finishing process suited to the specified floor tolerance. Timing matters. Concrete that is finished too early or too late can compromise the surface, while inconsistent placement practices can create localized deviations that remain after curing.
For existing facilities, the first question is whether the slab can be upgraded to meet VNA requirements. High-definition floor surveying identifies the condition of the intended wheel paths and reveals where corrective grinding, localized repair, joint work, or other remediation may be appropriate. Not every existing slab is a candidate for conversion. The available slab thickness, reinforcement, joint layout, moisture condition, surface integrity, and required correction depth must all be evaluated.
Grinding can be highly effective when it is used with a measured plan. It removes high areas and refines travel paths without unnecessary disturbance to the wider warehouse floor. However, grinding alone cannot solve every condition. A low area cannot be ground away, and widespread profile variation may call for a different corrective strategy. The right answer depends on verified data, not visual inspection.
Joints Are a Critical VNA Flooring Decision
Joints are often the first points of deterioration in heavy warehouse traffic. When truck wheels repeatedly cross an unprotected or failing joint, edges can break down, creating impact, vibration, and progressive spalling. In VNA aisles, that damage directly affects travel quality and can interfere with the tolerance the floor was intended to maintain.
Jointless or reduced-joint floor designs can limit the number of wheel impacts in critical travel zones. Where joints remain necessary, their location and treatment should be planned around the aisle layout whenever possible. Durable joint repair and protection systems help maintain the floor edge under repeated hard-wheel traffic.
The objective is not simply to make joints look clean at turnover. It is to create a floor that holds its profile under operational loading. A poorly repaired joint may pass a visual inspection but fail quickly once VNA trucks begin repetitive travel. Materials, preparation, cure time, and edge geometry all affect the repair outcome.
Surface Durability Still Matters
Flatness is central to VNA performance, but it is not the only requirement. Warehouse floors must also resist abrasion from tires, turning traffic in cross aisles, pallet movement, dropped loads, and cleaning activity. In some operations, they may need additional resistance to oils, chemicals, or washdown exposure.
The finish system should fit the use of the space. A dry, high-throughput distribution aisle has different demands than a food or beverage facility with regular sanitation. A floor finish selected only for appearance can create a maintenance burden if it does not match the traffic and exposure conditions.
Traction also requires careful judgment. The floor needs a profile suitable for the operation without creating a surface that is difficult to clean or unnecessarily aggressive on tires. This is one reason material selection should follow an operational review rather than a generic product preference.
Verification Should Be Part of Delivery
VNA flooring should be measured, documented, and evaluated against the agreed acceptance criteria. Verification is not an administrative step at the end of the project. It is how the team confirms that the delivered floor supports the equipment and rack system it was designed to serve.
Testing should focus on the relevant travel paths, not just random areas that may not represent operating conditions. The documentation should identify the measurement method, the areas tested, the results, and any completed corrective work. This gives the owner a clear record for commissioning, future maintenance, and coordination with equipment providers.
Where wire guidance is included, functional testing should confirm continuity and truck response before the aisle is released for service. It is far easier to resolve an issue before racks are fully loaded and operations are underway.
Plan Work Around Operational Uptime
Many VNA floor upgrades occur in active warehouses where shutdown windows are limited. That makes sequencing as important as the technical solution. Work areas may need to be isolated by aisle, phased by shift, or completed around receiving and shipping schedules. Dust control, access management, cure requirements, and protection of adjacent inventory must be built into the plan.
A fast installation that creates premature traffic damage is not a successful installation. The better approach is to define realistic access windows, protect the work from interference, and return each area to service only when it is ready for its intended loads.
Osis Group approaches superflat floors, wire guidance, grinding, and joint repair as connected elements of warehouse performance. The standard is not a surface that merely looks finished. It is a verified floor system that supports reliable travel where the operation has the least room for error.
Before committing to a VNA installation or conversion, put the truck wheel paths, lift heights, guidance requirements, and existing slab condition on the same drawing. That early coordination is often the most valuable correction a facility can make.


